DeepLink delivers end-to-end custom stainless steel tube fabrication and deep-drawn stainless steel components for industrial fluid handling, water filtration, and chemical processing equipment. Operating from an ISO 9001:2015, ISO 14001, and ISO 45001 certified 5,000+ m2 processing workshop with 10+ years of industry experience, 100+ professional staff, and 6+ automated production lines (80% automation level), DeepLink integrates rotary laser tube cutting, deep drawing, CNC machining, TIG welding, and heavy-duty bracket bending under one roof. Every order undergoes 39+ quality inspection checks, complies with SGS, ROHS, and REACH standards, and supports 2-3 day rapid prototyping with no minimum orders (No MOQ). (Note: Specific project parameters below, such as pipe wall thickness and pressure ratings, represent illustrative industry-standard benchmarks that are customized to exact client CAD drawings.)
1. Project Background & Fluid System Engineering Challenges
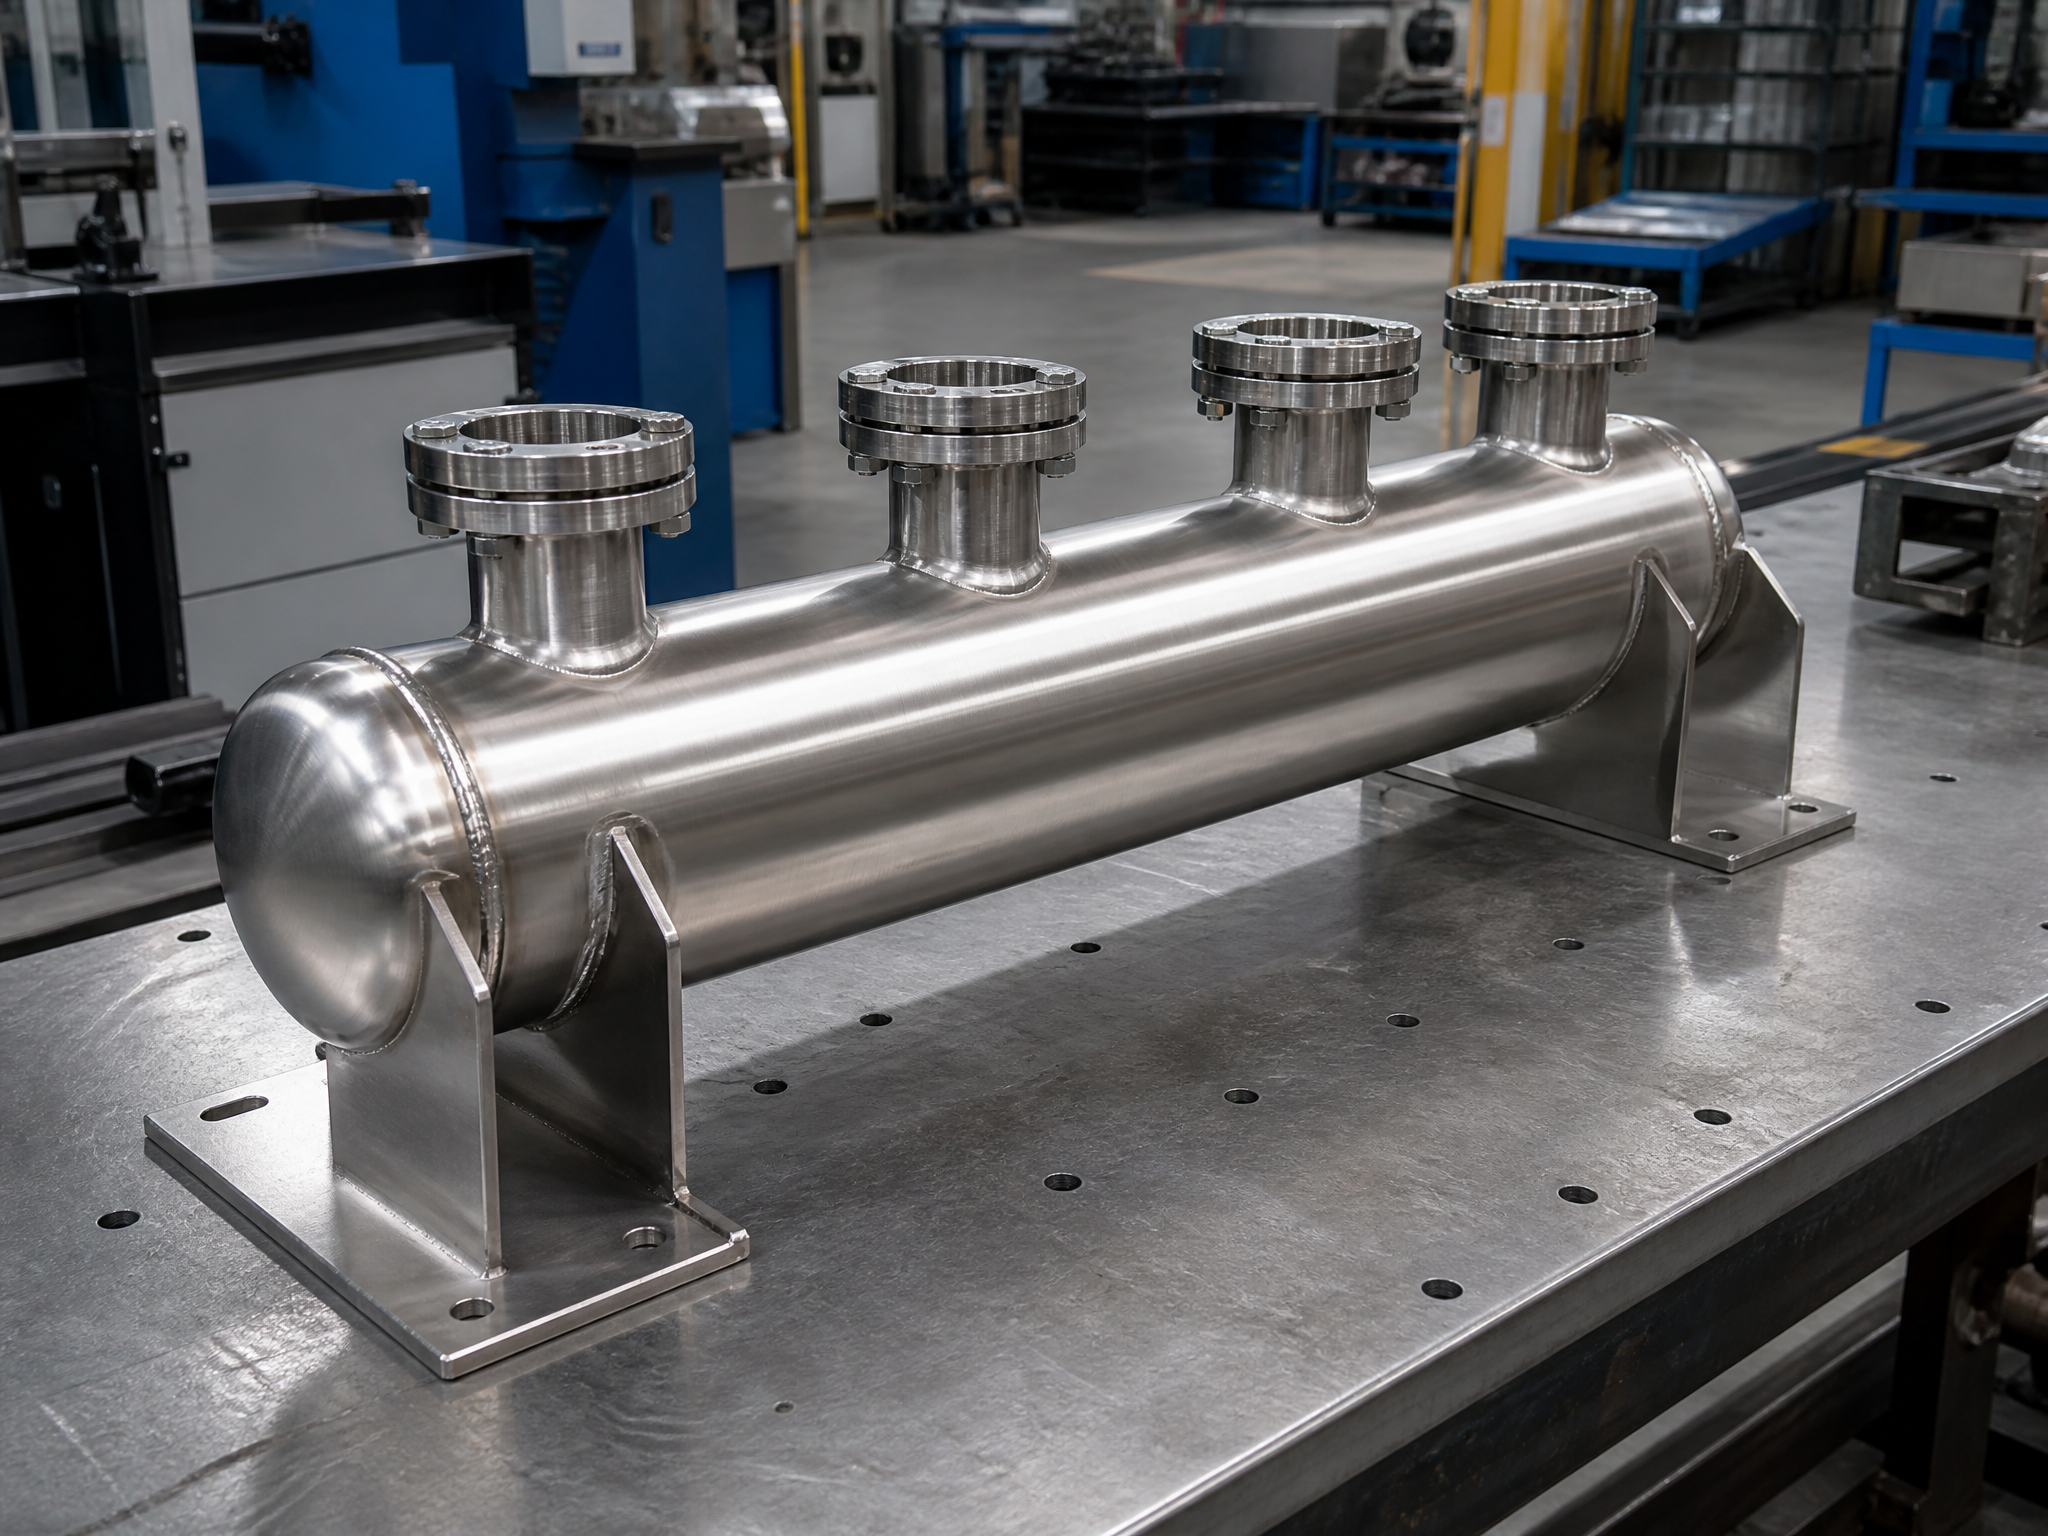
Industrial filtration skids, reverse osmosis (RO) plants, and sanitary fluid systems rely on multi-port distribution headers. Recently, an industrial water treatment equipment manufacturer approached DeepLink Metal Fab. They needed a single-source partner for custom stainless steel tube fabrication and modular manifold assemblies.
Previously, the client purchased raw pipes, stamped end caps, and CNC-machined flanges from three separate vendors. However, this multi-vendor workflow created serious assembly and reliability issues.
Specifically, the client faced four critical manufacturing challenges:
- Saddle Joint Misalignment: Conventional saw cutting and manual drilling produced uneven branch cutouts on the main header tube. Consequently, welding gaps varied and caused fluid turbulence.
- Leak Risks at Welded End Caps: Flat plate welded end caps trapped stagnant liquid and suffered from weld-toe corrosion under continuous pressure cycles.
- Chloride Pitting Corrosion: High-salinity water environments attacked standard carbon steel and unpassivated welds. Therefore, the system required marine-grade 316L stainless steel and full post-weld passivation.
- Mounting Frame Vibration: Heavy fluid manifolds vibrated during high-pressure pump cycles. As a result, they needed rigid, CNC-bent sheet metal support brackets that aligned accurately with the skid frame.
2. DeepLink’s Integrated Tube, Deep Drawing & Sheet Metal Solution
To eliminate supplier handoffs, our engineering team consolidated every process inside our 5,000+ m2 processing workshop. First, our engineers analyzed the client’s 3D STEP and SLDPRT assemblies and provided instant Design for Manufacturability (DFM) feedback.
Rotary Fiber Laser Tube Cutting for Intersecting Saddle Cuts
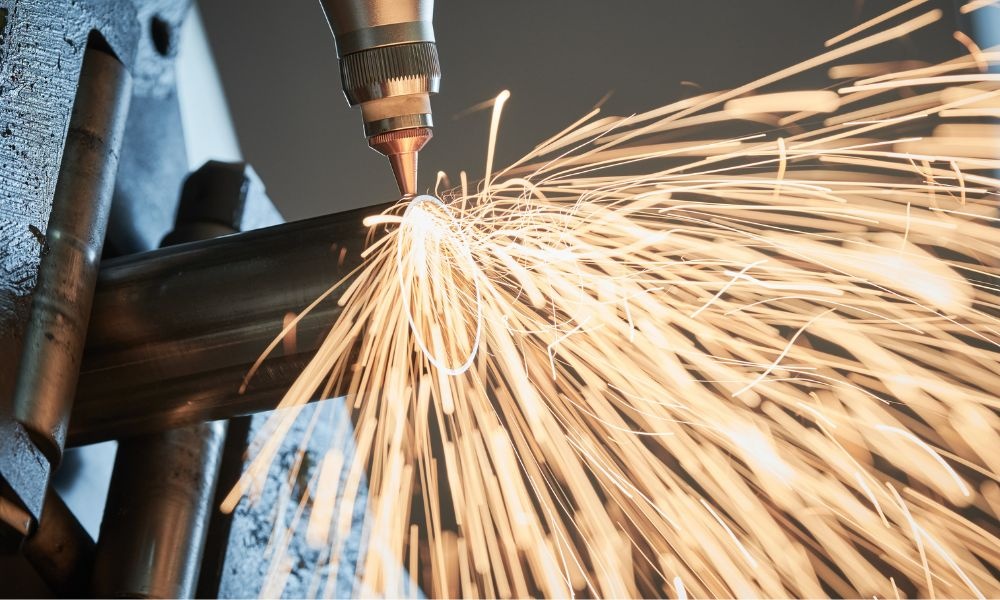
Accurate fit-up is the foundation of leak-free tube welding. Therefore, we utilized CNC rotary fiber laser tube cutting machines to process the 316L stainless steel main header pipes and branch outlets. Specifically, the rotary laser cut complex 3D intersecting saddle profiles (“fish-mouth” joints) directly into the branch tubes. Because the laser maintains tight positional accuracy, the branch outlets seated flush against the main header without manual grinding.
Seamless Deep-Drawn Stainless Steel End Caps
Instead of welding flat circular plates onto the manifold ends, we leveraged our in-house deep drawing presses. We formed seamless, hemispherical deep-drawn stainless steel end caps from 316L sheet stock. Furthermore, hemispherical caps distribute internal fluid pressure evenly and eliminate sharp dead-zone corners. In addition, a single circumferential butt weld joins each deep-drawn cap to the main tube, which significantly reduces welding distortion and leak paths.

Argon-Back-Purged TIG Welding & CNC Machined Flanges
High-purity fluid manifolds cannot tolerate internal weld oxidation (“sugaring”). Consequently, our certified welders executed full-penetration TIG welding while purging the interior of the 316L tubes with high-purity argon gas. This technique created smooth, sanitary root welds inside the pipe.
Simultaneously, our CNC machining department turned and drilled heavy-duty stainless steel outlet flanges. We designed each flange connection with a balanced, four-bolt pattern to guarantee uniform gasket compression while keeping maintenance access fast and uncluttered.
Sheet Metal Support Brackets & Passivation Finishing
To anchor the manifold assembly onto the client’s filtration skid, we laser-cut and formed heavy-gauge stainless steel saddle brackets using multi-axis CNC press brakes. Finally, the complete welded manifold underwent chemical acid pickling, passivation, and bead blasting. As a result, the passive chromium-oxide layer was fully restored across all heat-affected weld zones.
3. Verified Factory Capabilities & Illustrative Engineering Matrix
Every production batch at DeepLink Metal Fab undergoes 39+ quality inspection checks backed by ISO 9001:2015, ISO 14001, ISO 45001, SGS, ROHS, and REACH certifications. Below is a breakdown of our verified factory capabilities alongside illustrative engineering benchmarks for custom tube and manifold projects:
(Note: Quantitative factory data is verified from DeepLink’s official production profile; specific part dimensions and surface roughness values below serve as illustrative industry benchmarks and can be tailored to your exact blueprint [or replaced with your project specs].)
| Parameter Category | Verified DeepLink Capability / Illustrative Project Benchmark | Quality Control & Standard |
|---|---|---|
| Factory Infrastructure | 5,000+ m2 Workshop, 6+ Automated Production Lines (80% Automation Level), 100+ Professional Staff | 10+ Years of Industry Experience, Zero Handoffs |
| Core Integrated Processes | Rotary Laser Tube Cutting, Deep Drawing, Progressive Die Stamping, CNC Machining, CNC Bending, TIG/MIG Welding | Fully In-House One-Stop Manufacturing |
| Supported Materials | Stainless Steel (304 / 316L), Aluminum, Carbon Steel, Galvanized Sheet Metal | SGS Material Verification, ROHS & REACH Compliant |
| Accuracy & Tolerance | Official platform precision up to ±0.1” Accuracy (Illustrative CNC/Laser feature benchmark: [e.g., ±0.05 mm to ±0.15 mm per drawing]) | 3D Optical Inspection & Coordinate Measuring |
| Tube & Cap Geometry | Illustrative benchmark: [e.g., OD 25 mm – 150 mm tubes; 1.5 mm – 4.0 mm wall thickness] | Ultrasonic Wall Thickness & Fit-Up Gauges |
| Surface Treatments | 8+ Professional Finishes including Acid Pickling & Passivation, Brushed Finish, Bead Blasting, Electropolishing, Powder Coating | 39+ Quality Inspection Checks & Hydrostatic Leak Testing |
| Prototyping & Scaling | 2-3 Day Rapid Prototyping (No Minimum Orders / No MOQ) to Millions of Parts Annually | ISO 9001:2015, ISO 14001, ISO 45001 Certified |
| Accepted CAD Formats | STEP, STP, SLDPRT, STL, DXF, CATPART, PRT, SAT (10+ formats) |
Instant Digital Quoting & 24h DFM Feedback |
4. Related Industrial Applications & Internal Resource Links
Because DeepLink combines sheet & tube fabrication, CNC machining, and high-volume metal production on a single platform, engineering teams frequently bundle tubular assemblies with structural frames and enclosures:
- Heavy-Duty Skid & Conveyor Structures: Pair your fluid manifolds with our Heavy-Duty Structural Frames for Warehouse Automation and Conveyor Systems or Heavy-Duty Seismic Roof Mounting Brackets for Commercial HVAC Systems.
- Liquid-Cooled Data Centers & Outdoor Enclosures: Stainless steel coolant distribution manifolds integrate directly with our High-Density Data Center Server Racks and Modular Cold Aisle Containment and IP65 Weatherproof Metal Enclosures for Outdoor EV Charging Stations.
- Lightweight Precision Assemblies: Explore how we combine sheet metal forming with 5-axis milling in our High-Precision Aluminum Chassis for Industrial UAVs and Agricultural Drones.
- Platform & Engineering Guides: Compare factory-direct manufacturing against broker platforms in Deeplink vs Xometry: Which Custom Metal Fabrication Platform is Right for You in 2026? and review our DFM best practices in The Complete Guide to On-Demand Sheet Metal Fabrication (2026).
5. Frequently Asked Questions (FAQ)
What are the advantages of combining rotary laser tube cutting with deep-drawn end caps?
Why is 316L stainless steel recommended for welded tubular manifolds?
Does DeepLink require a minimum order quantity (MOQ) for custom tube and sheet metal assemblies?
How can I get DFM feedback and a quote for a custom tube or manifold project?
6. Start Your Custom Tube & Sheet Metal Project Today
From laser-cut tubular manifolds and deep-drawn stainless steel shells to heavy-duty mounting brackets, DeepLink Metal Fab handles your entire project in-house with zero handoffs. Upload your STEP, SLDPRT, or DXF files today for fast DFM feedback and factory-direct pricing.
Request Your Custom Metal Fabrication Quote in 24 Hours or email our engineering team at business@deeplinkpro.com.